Ricon Tools
Selecting the right shank is not a minor purchasing decision. It affects rigidity, indexing accuracy, tool life, and operator safety.
The question “how to select the correct vdi tool holder shank size” begins with the machine turret. Check the turret manual, machine plate, or certified drawing. Confirm the VDI standard, shank diameter, clamping method, tool orientation, and maximum supported holder length. DIN 69880 and ISO 10889 provide the dimensional framework, but machine-specific tolerances still matter. A VDI 30 holder cannot be treated as a smaller version of VDI 50. Their stiffness, clamping area, and vibration behavior differ.
Tony Schmitz, a recognized machining-dynamics researcher, states, “The machine tool, cutting tool, and workpiece form a dynamic system.” That principle explains why shank size must match the entire setup. AMT’s U.S. Manufacturing Technology Orders reports and Gardner Intelligence’s World Machine Tool Survey both document a broad mix of turning centers and automated production systems. This variety makes one-size-fits-all advice unreliable. It is also worth reading the tooling guidance from Sandvik Coromant, Seco, and ISCAR before purchasing.
Measure twice.
Use the largest compatible shank only when the turret, clearance, and operation allow it. Larger is not automatically better. A long holder, weak clamping, or poor alignment can still produce chatter. I have seen specifications appear correct on paper, yet fail during heavy interrupted cuts. That uncomfortable detail matters. The final choice should combine standard dimensions, actual machine documentation, cutting-force requirements, and a controlled test cut. Documentation is evidence; machining results are the final check.
How to Select the Correct VDI Tool Holder Shank Size?
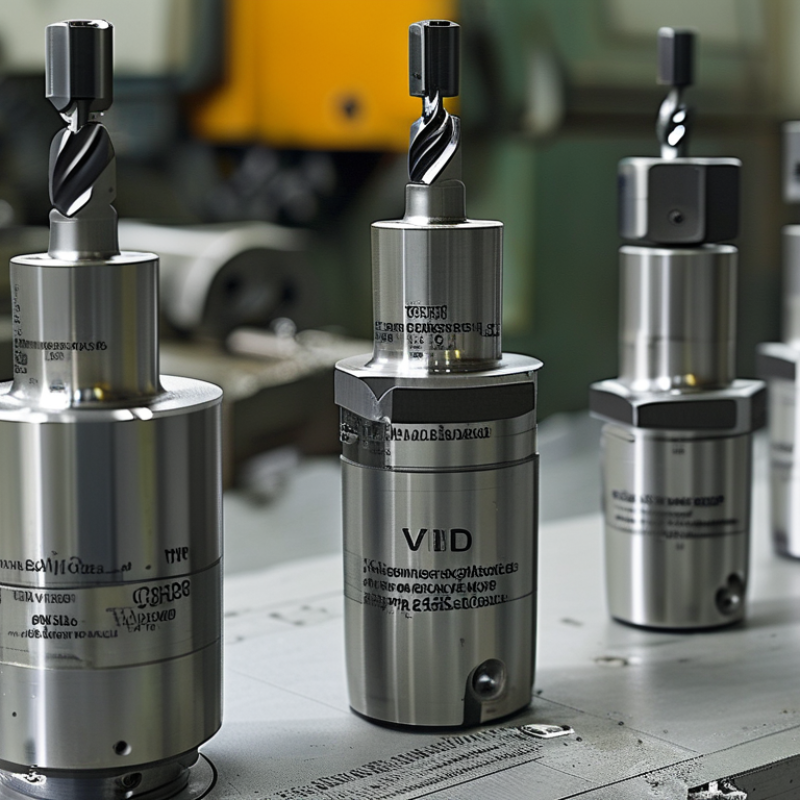
VDI tool holder shank size describes the holder’s nominal interface diameter and turret connection. It is not the cutting tool diameter. Common sizes include VDI 20, 30, 40, and 50. Larger numbers generally provide more stiffness, but they also require a matching turret and machine envelope. DIN 69880 defines key dimensional principles for these holders, helping manufacturers maintain interchangeability across compatible systems.
Selection should begin with the lathe model, turret specification, and machining load. A VDI 30 holder may suit light turning and compact machines, while VDI 40 or VDI 50 can better resist deflection during heavy roughing. Check the turret bore, clamping method, gauge length, coolant path, and interference around the workpiece. A longer holder can reach a deep shoulder, but it may amplify vibration. Short is often safer.
Automation makes consistency more important. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023. That growth reflects tighter demands for repeatable setups and reliable tool changes. In practice, measure the turret socket instead of trusting a worn label. Then verify the holder drawing and tolerance. Mistakes happen. I once treated shank size as a tool-diameter choice; that shortcut ignored the machine interface and created unnecessary setup risk. Check twice.
How to Select the Correct VDI Tool Holder Shank Size?
Identify the machine interface before choosing a shank. VDI tooling commonly follows DIN 69880, with sizes such as VDI 30, VDI 40, and VDI 50. These numbers describe the machine’s interface class, not a universal diameter measurement. Check the turret drawing, locking method, key position, and available clearance. A VDI 40 holder will not safely replace a VDI 30 holder. The mismatch may look minor, but it can create runout, vibration, or poor repeatability. Grand View Research estimated the global CNC machine market at about USD 88.6 billion in 2023, with a projected 6.3% annual growth rate through 2030. That expansion makes interface accuracy more important across mixed machine fleets.
Confirm the VDI standard from the machine manual or turret plate. Do not rely only on a photograph. Some machines use BMT or other interfaces, even when the holder appears similar. Measure the locating diameter and inspect the clamping face. In practical checks, a small burr can prevent full seating. I have seen operators blame cutting data when the real problem was an incorrect shank size. That is an easy mistake. It still happens.
Tips: Record the machine model, turret interface, VDI size, holder orientation, and coolant arrangement. Ask the tooling supplier for a dimensional drawing. Compare every critical measurement before ordering. If the drawing is unclear, stop and verify it. Guessing is cheaper only until the first failed setup.
Selecting a VDI tool holder shank starts at the turret, not the cutting tool. The shank diameter must match the station bore and clamping system specified for your lathe. Measure the turret interface carefully, including the locating shoulder, keyway position, and available insertion depth. Common nominal sizes may look similar, but a small mismatch can prevent full seating. That matters.
Use the machine manual as the primary reference, then verify the physical dimensions. A vernier caliper helps with screening, but a micrometer provides better confidence. Check the shank diameter, tolerance, clamping length, and shoulder position. Also inspect the station’s orientation feature. A holder can fit the bore yet sit incorrectly against the turret face. This may shift the cutting edge from the programmed centerline.
Leave enough clearance for the tool body, coolant fittings, and adjacent stations. Dry-fit the holder before installing an insert or expensive cutting tool. Look for rocking, uneven contact, or a key that does not fully engage. Do not force it. Even experienced machinists sometimes trust a familiar size without checking the actual turret. I have seen measurements taken from an old holder instead of the machine interface. That shortcut can mislead. Record the verified dimensions for future setups, and recheck them after turret maintenance or replacement.
Selecting a VDI tool holder shank size starts with rigidity, not convenience. A larger shank generally resists bending and torsional movement better. Published machining studies in CIRP journals show that cutting-force deflection rises sharply as tool overhang increases. In simplified beam models, deflection can increase with the cube of unsupported length. Small changes matter.
Measure the actual reach from the turret face to the cutting edge. For a short turning operation, select the largest shank that fits the VDI turret pocket. For deep bores, shoulder work, or interrupted cuts, avoid solving reach problems with excessive extension. A 20% increase in overhang can create far more vibration than expected. That relationship is easy to underestimate.
Machining requirements should decide the compromise. Heavy roughing needs maximum cross-section and secure clamping. Finishing may tolerate a smaller shank when access and visibility improve. ISO 26623-1 provides dimensional guidance for polygonal tool interfaces, while ISO 230-2 testing principles remind users that machine accuracy and setup stability affect results. Industry cutting-tool reports from the U.S. Cutting Tool Institute recorded billions of dollars in annual tool consumption, reflecting how costly repeated tool changes can become. Measure twice.
In practice, check spindle power, insert size, coolant access, turret clearance, and expected chip load. A rigid holder can still fail when the insert geometry is too aggressive. That part is often overlooked. Trial cuts should compare flank wear, surface finish, sound, and spindle load. Do not trust rigidity claims alone. Your machine, fixture, and workpiece may disagree.
Evaluate rigidity, reach, and machining requirements before selecting a nominal shank diameter. Bending stiffness increases approximately with the fourth power of diameter, so larger shanks provide substantially greater resistance to deflection when the holder and machine interface are compatible.
Reading the chart: The relative bending-stiffness index is calculated from (shank diameter ÷ 16 mm)4, using a 16 mm shank as the baseline. Use smaller shanks for short-reach, light-duty work and larger shanks when long reach, heavy cutting, high feed rates, or vibration control are required. Actual selection must also consider machine compatibility, holder geometry, tool mass, and the cutting force of the operation.
Selecting a VDI tool holder shank starts with the machine turret, not the cutter. Check the turret specification, shank size, flange geometry, and gauge length. DIN 69880 defines common VDI interface dimensions, but nominal size alone does not confirm compatibility. Measure twice.
Verify the clamping diameter with a calibrated gauge. Then inspect the locating shoulder, key position, coolant passage, and nearby turret clearance. A VDI 30 holder may fit the bore yet interfere with the turret body or workpiece. Check tool offset limits before installation. The 2024 CNC Machine Tools Market Report projects about 6% annual market growth through 2030, increasing the need for repeatable, interchangeable tooling. However, market growth does not guarantee standardization across every machine.
Compatibility also depends on the cutting tool connection. Confirm the holder’s collet, insert pocket, boring bar diameter, and maximum speed. Compare the holder drawing with the machine manual, including pull-in direction and indexing requirements. I have seen technicians verify the shank but overlook the coolant port. That small mistake caused poor chip evacuation. Record measured runout at the gauge line, preferably below the machine builder’s stated limit. A checklist helps, but it is never perfect. Recheck clearance with the actual workpiece, tool projection, and guard closed.
: Start with the lathe turret, not the cutting tool. Match the shank diameter, bore, clamping system, and insertion depth.
Check the locating shoulder, keyway position, flange geometry, and orientation feature. Small differences can prevent full seating.
Yes. It may rock, contact unevenly, or sit incorrectly against the turret face. That can shift the cutting edge.
Use a vernier caliper for screening. Use a micrometer or calibrated gauge for closer dimensional checks.
Leave space for the tool body, coolant fittings, nearby stations, the workpiece, and the closed machine guard.
Dry-fit the holder before installing an insert or expensive cutter. Check for rocking, incomplete key engagement, and uneven contact.Do not force it.
No. Confirm the collet, insert pocket, boring bar diameter, coolant passage, maximum speed, and gauge length.
A misplaced or blocked port can reduce chip evacuation. It is a small detail, but easy to miss.
Record verified dimensions, tool offset limits, and gauge-line runout. Recheck them after turret maintenance or replacement.
Not always. Recheck the actual workpiece, tool projection, clearance, and clamping condition. Familiar dimensions can mislead.
Selecting the correct VDI tool holder shank size begins with understanding the holder’s function and the machine’s interface. The shank is the section that fits into the turret or tool station, so its dimensions must correspond precisely with the machine’s VDI standard, turret design, and station requirements. Before choosing a holder, confirm the machine model specifications, the applicable VDI size, insertion method, clamping arrangement, and available clearance. These details prevent installation problems and help ensure accurate tool positioning.
To determine how to select the correct vdi tool holder shank size, compare the shank diameter, length, orientation, and locating features with the turret and tool station. Then evaluate the required rigidity, cutting forces, tool reach, and machining conditions. A larger or more rigid holder may improve stability, while an unnecessarily long or oversized holder can reduce clearance and increase vibration. Finally, verify the complete tool holder compatibility, including clamping contact, coolant access, adjacent-station clearance, and alignment. Careful dimensional checks before purchase or installation support safer, more reliable, and more consistent machining performance.